Black Chromate Coating is a conversion finish applied mainly to zinc-plated steel, zinc die castings, and selected aluminum parts. It creates a dark, thin surface film rather than a thick decorative layer. Under workshop lighting, the result may appear jet black, charcoal, or slightly olive. That variation matters when buyers specify appearance without defining an acceptable color range.
Frank Altmayer, an AESF Fellow and long-time surface-finishing educator, states, “Surface preparation determines coating performance.” His point reflects daily production experience. Oil, fingerprints, poor rinsing, or uneven zinc thickness can produce cloudy patches and early corrosion. Black chromate coating is used on fasteners, brackets, automotive hardware, electrical components, and machinery parts requiring a low-reflective finish. It can also support paint adhesion and preserve electrical contact, depending on the complete finishing system.
The process normally includes cleaning, zinc plating, activation, chromate treatment, rinsing, and controlled drying. Sealers may improve corrosion resistance, but they can change conductivity, color, or friction. That trade-off is often overlooked. Older hexavalent systems may offer strong performance, while trivalent alternatives are increasingly selected for workplace and environmental compliance. Requirements differ by product, market, and jurisdiction, so technical data sheets and current regulations deserve careful review. This article examines how Black Chromate Coating works, where it performs well, and where its limitations become visible. It is not a universal black finish. Even experienced applicators can misjudge it when appearance receives more attention than pretreatment, film control, and service conditions.
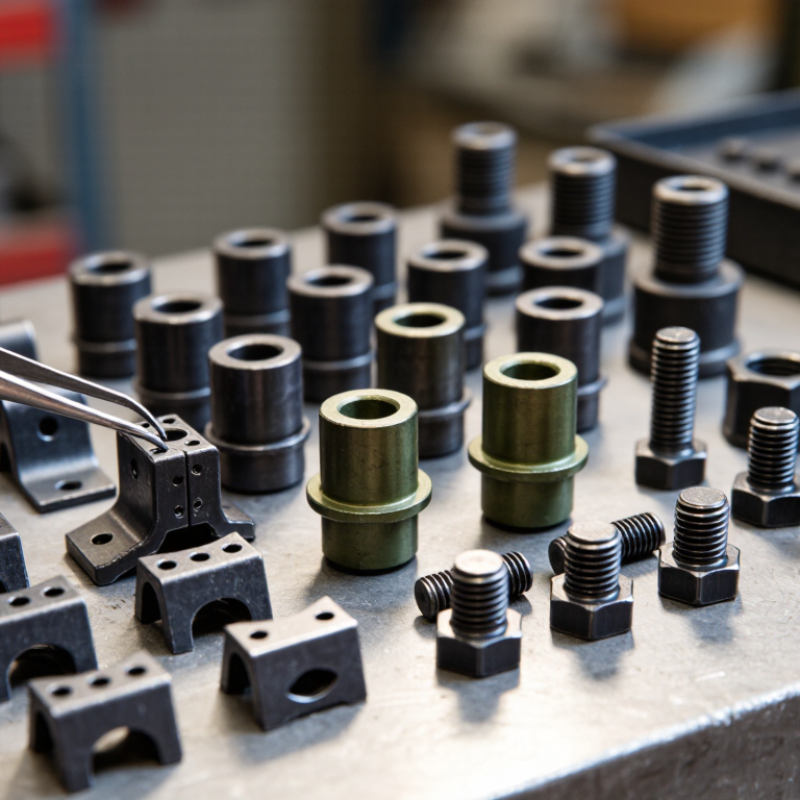
What Black Chromate Coating Is and How It Works
Black chromate coating is a thin chemical conversion layer applied mainly to zinc-plated steel. It changes the surface chemistry, rather than building a thick protective film. The treatment usually contains chromium compounds, additives, and controlled rinsing stages. Modern specifications often favor trivalent chromium systems, but the exact chemistry must be confirmed through the supplier’s technical data sheet.
The process begins with cleaning and activation. Zinc surfaces must be free from oil, fingerprints, and corrosion. After immersion or spraying, the conversion film forms microscopic compounds across the metal. These compounds improve corrosion resistance and create a dark, low-glare appearance. The coating also helps paint and sealants adhere.
It is not magic.
ISO 4520 covers chromate conversion coatings on electroplated zinc surfaces. ASTM B117 specifies a salt-spray test using a 5% sodium chloride solution at approximately 35°C. However, salt-spray hours do not equal real service life. Humidity, scratches, handling, and edge geometry can change performance significantly. This is where practical inspection matters.
Black chromate appears on fasteners, brackets, stamped components, electrical hardware, and automotive fittings. Designers choose it when appearance, moderate corrosion protection, and low thickness are important. The layer is typically far thinner than paint, so it rarely changes thread fit. Still, dark finishes can hide early white corrosion. That weakness deserves attention. Surface preparation and post-treatment control often matter more than color. USGS Mineral Commodity Summaries 2024 reported global zinc mine production near 12 million metric tons in 2023, supporting zinc’s continued industrial importance.
The Materials and Surface Preparation Used in Black Chromating
Black chromate coating is usually applied to zinc or zinc-alloy plated steel. The base metal matters. Zinc offers sacrificial corrosion protection, while the chromate film improves appearance and reduces early white corrosion. Black color comes from pigments, bath chemistry, and film structure, not from a thick paint layer. The conversion film is extremely thin, often below one micrometre, so scratches can expose the underlying zinc quickly.
Surface preparation decides the result. Operators normally remove oil with an alkaline cleaner, rinse with low-contamination water, then activate the zinc with a mild acid treatment. Even fingerprints can create pale stains or uneven black patches. ASTM B633 identifies common zinc coating thickness classes, including 5, 8, 12, and 25 micrometres. The chosen thickness should match the part’s environment and geometry. More zinc is not always better; trapped chemistry inside threads can cause defects.
Testing still needs careful interpretation. ASTM B117 uses a 5% salt solution at 35°C, but it does not predict exact outdoor service life. ISO 4520 also treats chromate conversion as a supplementary finish, not a replacement for sound zinc coverage. In production, technicians should inspect water-break behavior, coating continuity, color uniformity, and adhesion. A glossy black surface can look excellent and still perform poorly. That is the uncomfortable part. Gear edges, recesses, and poorly rinsed holes often reveal the real process quality.
The Step-by-Step Black Chromate Coating Process
Black chromate coating is a conversion finish commonly applied over zinc-plated steel. It creates a dark, thin surface film. The coating improves corrosion resistance and reduces the bright metallic appearance. It is not paint. Its final shade may range from charcoal to deep black.
The process begins with careful surface preparation.
Technicians remove oil, dirt, and polishing residue using an alkaline cleaner. The parts are rinsed thoroughly. Any residue can cause uneven color. An acid activation step then refreshes the zinc surface. Another rinse follows. Small details matter here. Poor rinsing is a common failure point.
The prepared parts enter a controlled black chromate bath for a measured time.
Operators monitor concentration, temperature, and immersion speed. Excessive processing can create stains or a powdery surface. After chromating, the parts receive several clean-water rinses. A sealant may be applied when specifications require stronger corrosion protection. The parts then dry at a controlled temperature, avoiding water spots.
Inspectors check color, coverage, adhesion, and corrosion performance. Test panels help confirm bath stability. In practice, perfect uniformity is difficult, especially around holes and sharp edges. That limitation deserves attention during design reviews. A qualified finishing facility should record each bath adjustment and inspection result.
Key Properties and Performance Benefits of Black Chromate
Black chromate coating is a thin conversion layer applied mainly over zinc-plated steel, aluminum, or related metal surfaces. It changes the surface chemically rather than adding a thick paint film. The result is a deep black or charcoal appearance with a slightly varied tone.
Its main value is functional. Black chromate can improve corrosion resistance, especially when combined with a suitable sealer. It also helps protect the underlying zinc from early oxidation during storage and handling. The coating remains thin, so threaded fasteners usually keep their fit. That matters in assemblies with tight tolerances.
The finish can reduce glare on exposed hardware. It is useful for automotive components, electrical enclosures, machinery parts, and visible fasteners. Some formulations preserve limited electrical conductivity, but this should be verified by testing. Color consistency depends on bath chemistry, rinsing, surface preparation, and immersion time. Small process changes can create gray, brown, or uneven areas.
It is not magic. Black chromate alone cannot replace sound plating or proper sealing. In practical inspections, I would check coating coverage, adhesion, color uniformity, and corrosion performance under the intended environment. Salt spray results are helpful, but they do not perfectly predict field service. Handling can also mark the surface, particularly before final sealing. Trivalent chromate systems are increasingly selected where reduced hazardous exposure and regulatory compatibility are important, though performance still depends on the complete finishing process.
Common Industrial Applications and Practical Limitations
What Is Black Chromate Coating and Where Is It Used?
Black chromate coating is a thin conversion layer applied mainly over zinc-plated steel. It creates a dark, low-reflective surface and improves initial corrosion resistance. The finish also reduces glare on brackets, fasteners, stamped parts, and equipment housings. Common users include automotive suppliers, electrical manufacturers, machinery builders, and hardware producers. Some electronics enclosures use it where appearance and moderate conductivity matter.
Practical limitations deserve closer attention. Black chromate is not a universal shield. Its protection depends on zinc thickness, sealing, handling, and exposure conditions. ASTM B117 salt-spray results can compare samples, but they cannot predict exact outdoor service life. A small scratch may expose zinc quickly, especially near sharp edges. Color can also vary between production batches. The boundary is not always clean.
Modern specifications often prefer trivalent chromium systems. Legacy hexavalent processes require strict industrial controls because OSHA limits airborne hexavalent chromium exposure to 5 micrograms per cubic meter over an eight-hour workday, under 29 CFR 1910.1026. The U.S. EPA’s 2023 TRI National Analysis continues to classify chromium compounds as reportable chemicals. Buyers should request chemistry declarations, coating thickness records, adhesion checks, and corrosion-test conditions. Do not judge quality by darkness alone. A very black surface may still have weak sealing or poor edge coverage. That detail is easy to miss.
What Is Black Chromate Coating and Where Is It Used?
Black chromate is a thin chemical conversion coating normally applied over zinc-plated steel, zinc die castings, and other zinc surfaces. It provides a dark appearance, limited corrosion protection, and improved surface passivation rather than acting as a thick standalone barrier.
Representative industrial thickness ranges are shown in micrometres (µm). Actual values vary with the zinc-plating specification, chromate chemistry, sealing process, and performance requirement.
Common Industrial Uses
Black chromate is commonly used on fasteners, brackets, stamped parts, automotive hardware, appliance components, electrical hardware, and zinc die-cast parts where a dark finish and moderate corrosion resistance are required.
Practical Limitations
The conversion layer is very thin and can be damaged by abrasion, forming, or aggressive handling. Appearance may vary with the zinc surface and bath condition. Legacy hexavalent-chromium processes are also restricted in many applications, so trivalent alternatives and sealers are increasingly specified.
Conclusion
Black Chromate Coating is a chemical conversion treatment used to create a dark, protective finish on metal surfaces, especially zinc and zinc-plated components. The process typically begins with cleaning, degreasing, rinsing, and activating the substrate so the coating can form evenly. The prepared part is then immersed in a chromating solution for a controlled period, followed by rinsing and drying. Depending on the required performance, a sealing or protective top treatment may also be applied.
This coating provides a low-reflective black appearance, improved corrosion resistance, and a useful base for further protection or identification. It is commonly used on fasteners, brackets, hardware, automotive components, electrical parts, and general industrial assemblies. However, its durability depends on the substrate, surface preparation, bath control, and handling conditions. Black Chromate Coating may offer less wear resistance than thicker painted or plated finishes, so it should be selected according to the component’s exposure, friction, appearance, and service requirements.
 HIYIE